Direct supply chain integration for professional workshop infrastructure, pneumatic support systems, and precision hardware tooling.
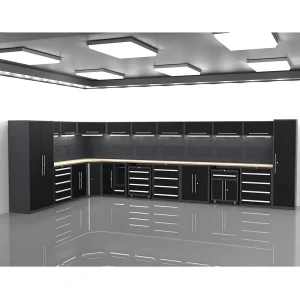


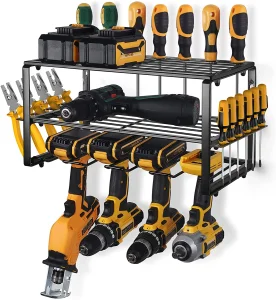
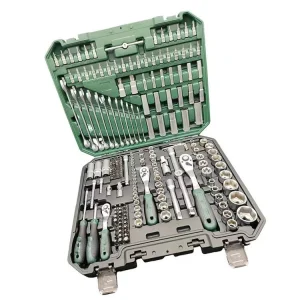
A comprehensive analysis of thermodynamic efficiency, OEM customization protocols, and smart factory integration.
In modern industrial manufacturing, compressed air is universally recognized as the "fourth utility" alongside electricity, water, and natural gas. As global industrial automation accelerates, the procurement paradigms for air compressor systems have shifted dramatically. B2B buyers, EPC contractors, and brand owners no longer search for off-the-shelf catalog machinery; instead, they demand tailored, high-efficiency, Custom OEM Air Compressor Solutions engineered for specific thermodynamic footprints, severe ambient conditions, and stringent power quality constraints.
The global industrial air compressor manufacturing domain is undergoing a dual transformation powered by decarbonization mandates (EU Stage V, US Energy Star, China GB19153 standards) and Industry 4.0 digitisation. Advanced Original Equipment Manufacturers (OEMs) and turnkey factories must combine ultra-precise mechanical machining with intelligent variable frequency control systems. The market demands bespoke compressed air infrastructure capable of delivering continuous volumetric efficiency across diverse operating pressures ranging from low-pressure 3-5 bar systems to high-pressure 40-300 bar multi-stage booster configurations.
Selecting an OEM partner requires looking beyond simple horse-power (HP) metrics. Evaluation must focus on Specific Energy Consumption (SER, measured in kW/m³/min), thermal dissipation management, rotor dynamic balance, and total cost of ownership (TCO) over a 15-year operational lifecycle.
How specialized manufacturing factories build customized pneumatic platforms for global brands.
Custom OEM factories utilize proprietary 5:6 or 4:6 asymmetric rotor tooth profiles. Machined on German CNC grinding systems, these rotors minimize internal gas recirculation losses, maximizing free air delivery (FAD) while reducing mechanical friction by up to 18%.
OEM solutions incorporate Permanent Magnet Variable Speed Drive (PM-VSD) motors featuring IE4 and IE5 super-premium efficiency ratings. Liquid-cooled motor housings prevent demagnetization under ambient temperatures exceeding 50°C.
For cleanroom environments such as pharmaceuticals, semiconductors, and food processing, OEMs produce dry scroll and water-injected rotary screw compressors certified to ISO 8573-1 Class 0, eliminating hydrocarbon contamination risks.
Bespoke canopy development tailored for extreme outdoor environments (IP54/IP65 ratings), featuring sound-attenuating polyurethane foams that drop operational noise levels down to 62 dB(A) for residential or indoor laboratory deployments.
Fully compliant vertical and horizontal air receiver tanks, certified against ASME Section VIII Div 1, PED 2014/68/EU, and DOSH standards, customized with anti-corrosion epoxy interior linings.
Integration of heavy-duty aluminum plate-fin oil coolers and shell-and-tube heat exchangers with dynamic bypass thermal valves, preventing moisture condensation inside lubrication circuits.
| Compressor Technology Type | Pressure Range (Bar) | Flow Rate Range (FAD m³/min) | Oil Purity Level | Target OEM Applications |
|---|---|---|---|---|
| Direct-Drive Rotary Screw | 7.0 - 13.0 Bar | 0.8 - 65.0 m³/min | Oil-Injected (< 3ppm) | Heavy Plant Manufacturing, Mining, General Industrial |
| Two-Stage Oil-Free Screw | 4.0 - 10.5 Bar | 5.5 - 45.0 m³/min | ISO 8573-1 Class 0 | Pharmaceutical Cleanrooms, Electronics, Food & Beverage |
| Permanent Magnet VSD Screw | 6.0 - 15.0 Bar | 0.3 - 30.0 m³/min | Oil-Injected (< 2ppm) | Automotive Workshops, Laser Cutting, Textiles |
| High-Pressure Reciprocating | 30.0 - 350.0 Bar | 0.1 - 8.0 m³/min | Oil-Lubricated / Dry | PET Bottle Blow Molding, CNG Stations, Valve Testing |
| Silent Compact Scroll | 8.0 - 10.0 Bar | 0.2 - 2.4 m³/min | ISO 8573-1 Class 0 | Medical Dental Clinics, Analytical Labs, Printing Presses |
Combining 15 years of hardware legacy with advanced motor winding, precision turning, and digital QA inspection.
A reputable OEM factory’s core strength lies in its vertical integration. Building reliable industrial hardware—ranging from heavy-duty workshop tool chests and precision metalworking boring bars to complex rotary compressor drive motors—requires rigorous quality control across every mechanical process step.
Derived from nearly 15 years of deep hardware tooling operations, our integrated manufacturing ecosystem incorporates state-of-the-art motor fabrication, automated winding systems, precision finish turning (FT), dynamic spot welding, and strict end-of-line thermodynamic testing.
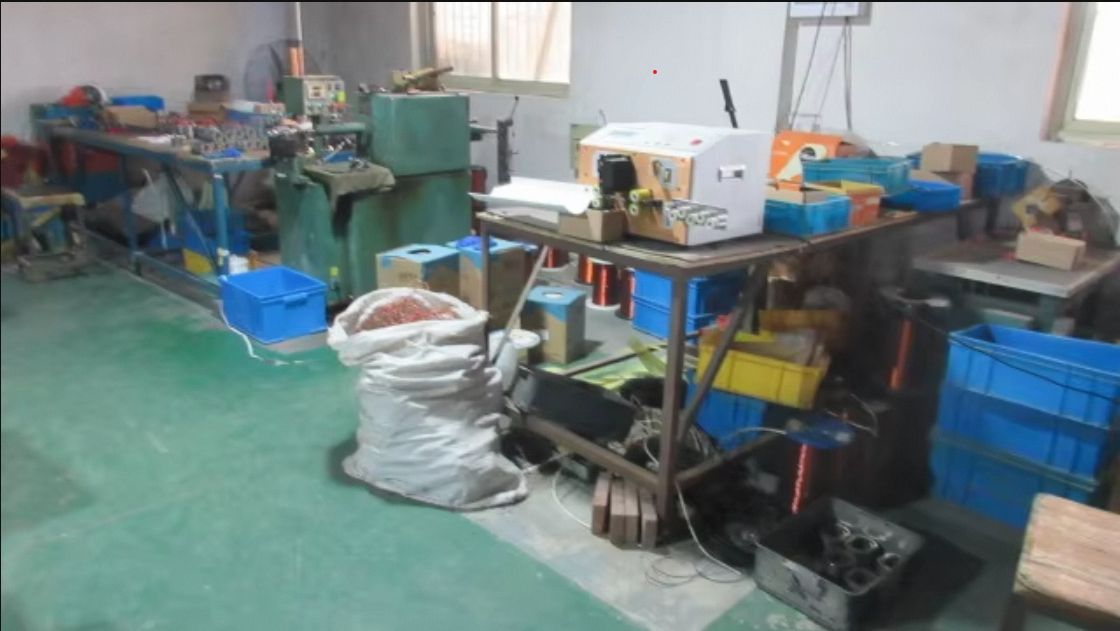
High-precision stator copper coil wrapping for maximum electromagnetic conversion efficiency.
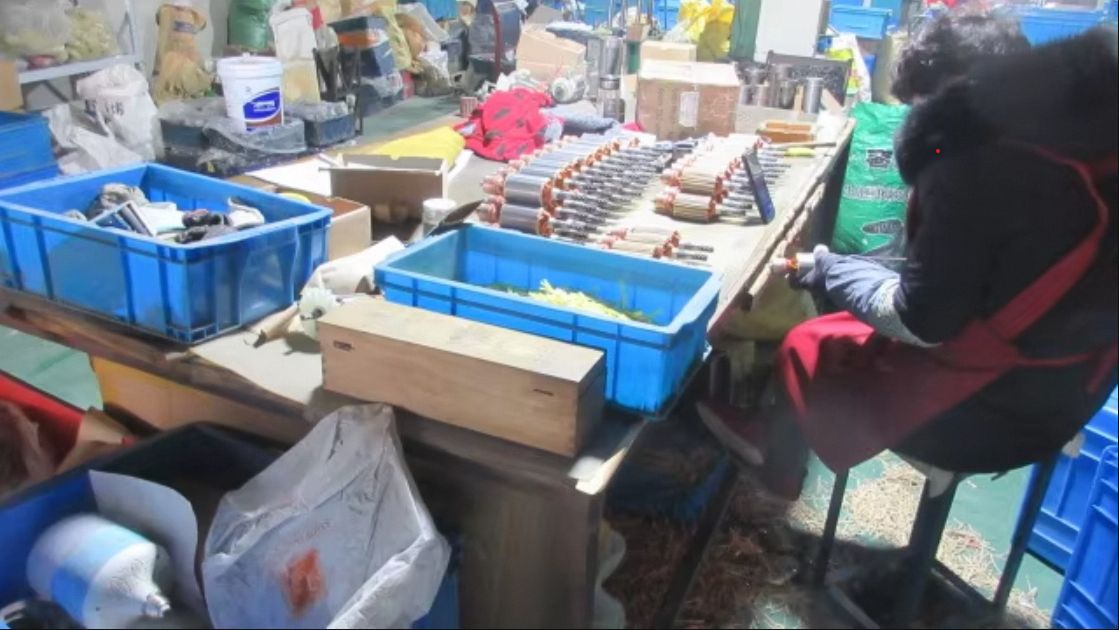
Automated slot insulation insertion securing dielectric strength across heavy thermal cycles.
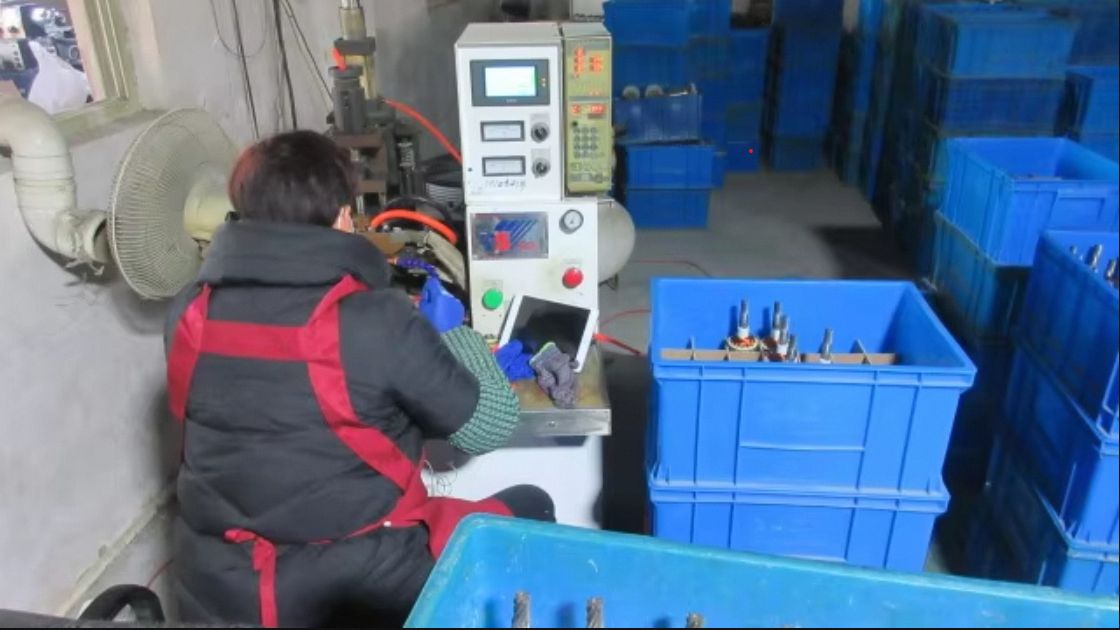
Micro-processor controlled welding ensuring ultra-low contact resistance across motor leads.
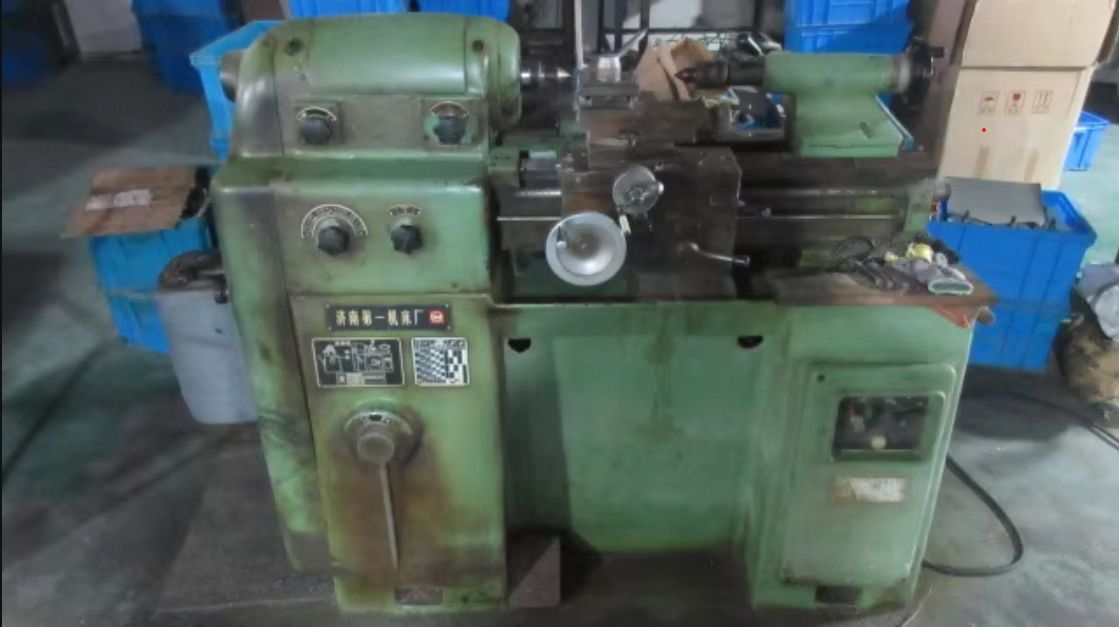
Sub-micron CNC shaft turning ensuring zero vibration during 10,000+ RPM rotor rotation.
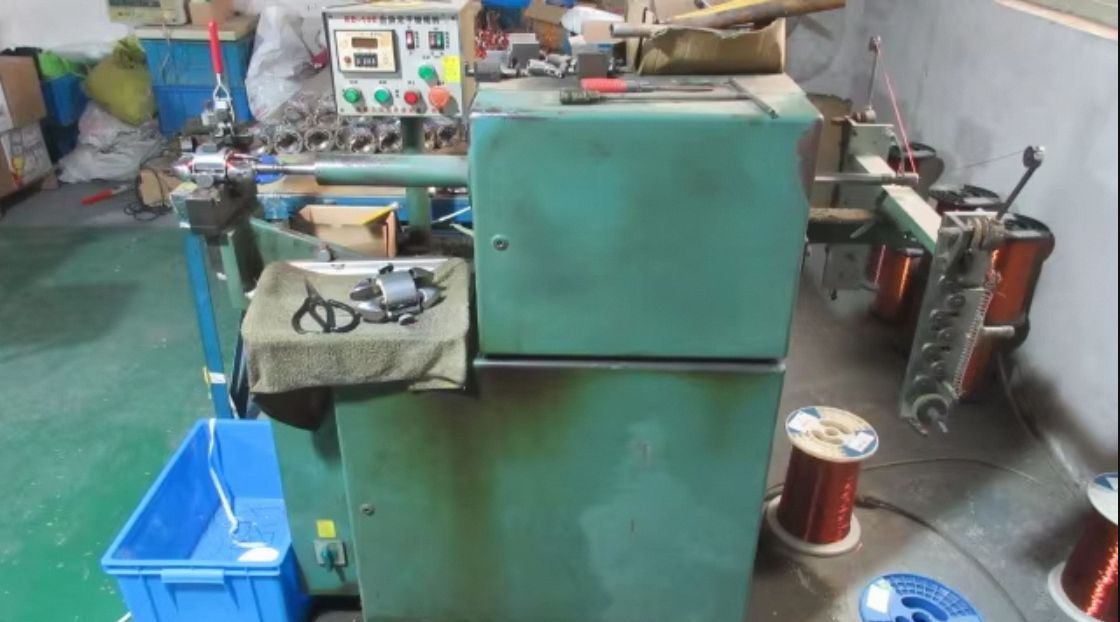
Multi-axis CNC coil winders achieving dense copper slot fills for high power density.
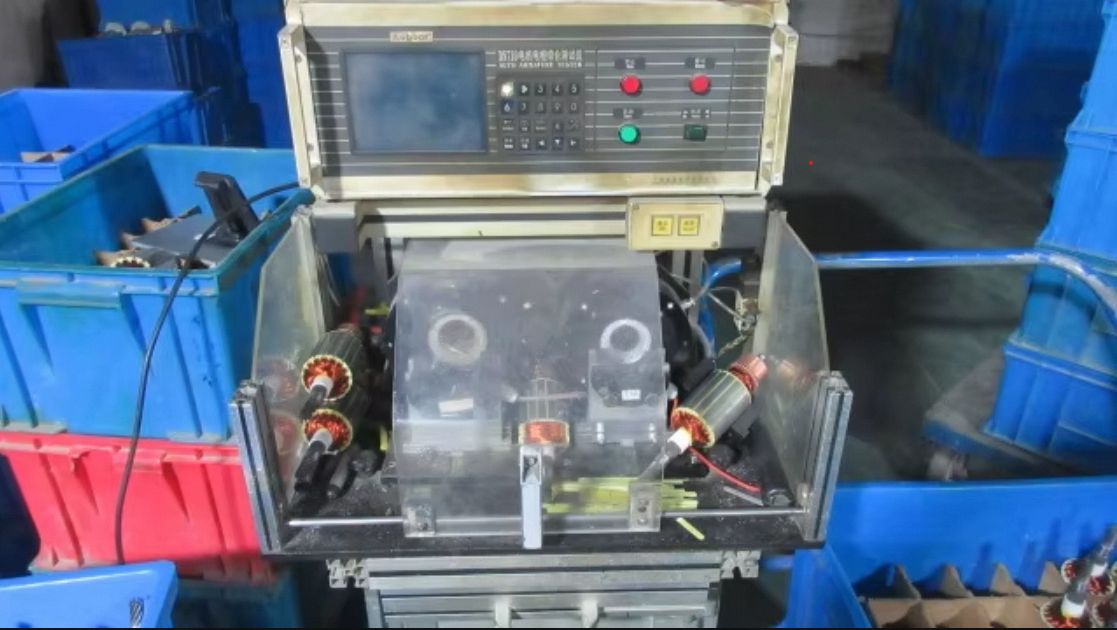
100% full-load thermal run testing, insulation breakdown analysis, and acoustic profiling.
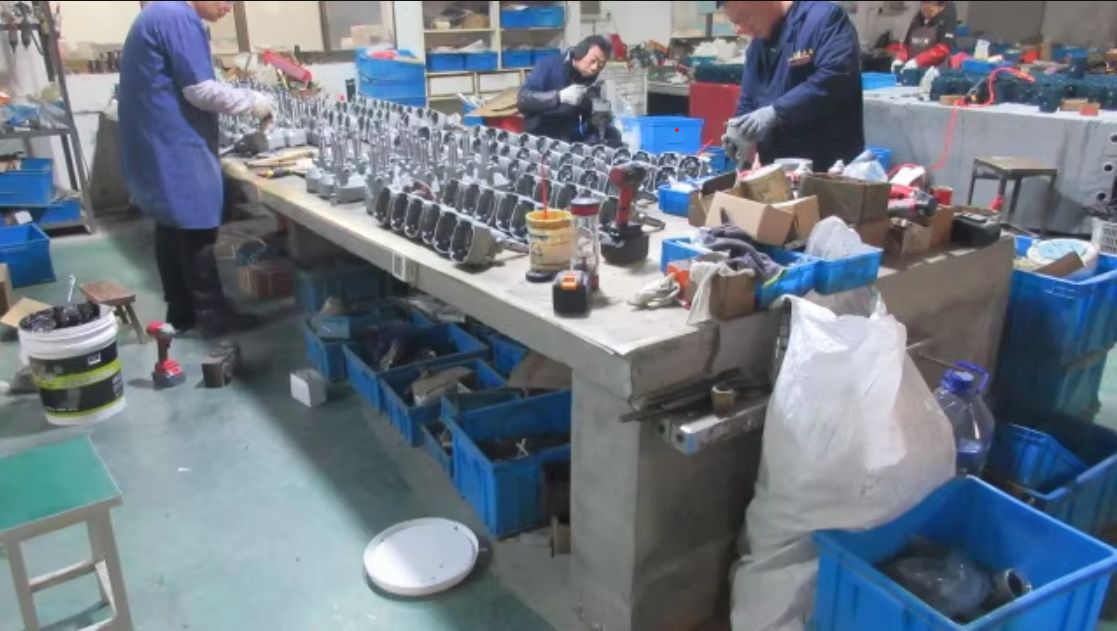
Clean-room assembly of airends, VFD units, pressure vessels, and control cabinets.
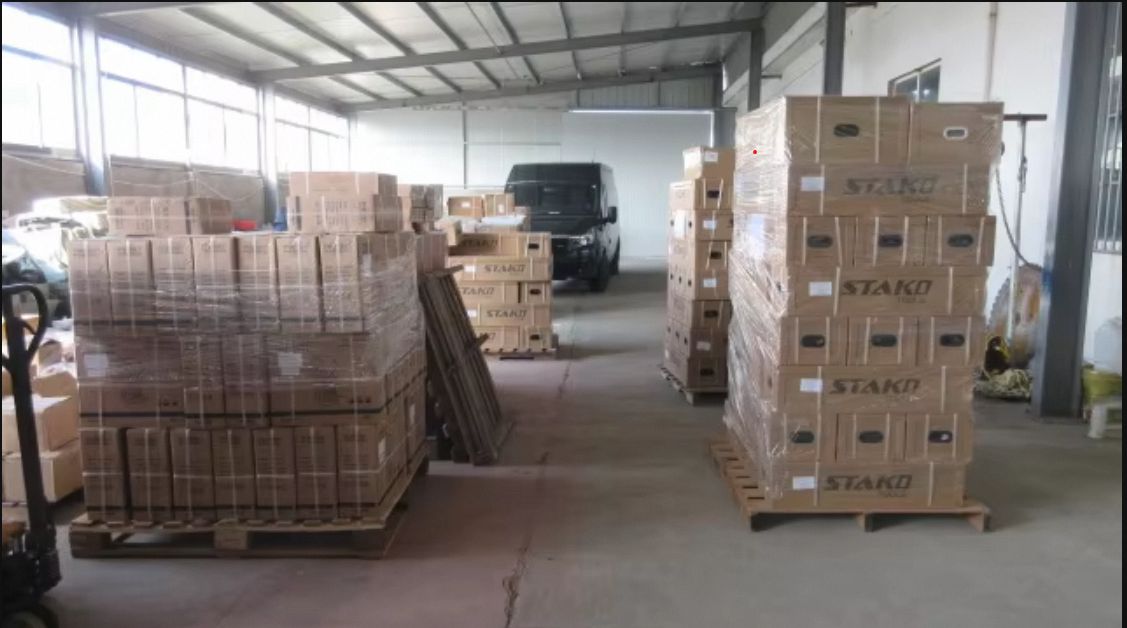
Export-ready protective packaging with full compliance documentation and factory test reports.
Established as a modernized hardware and machinery enterprise in 2023, Zhejiang Pargo Tool Co., Ltd. builds upon nearly 15 years of accumulated manufacturing expertise. Operating an extensive multi-category footprint spanning hardware tools, power equipment, automotive garage systems, and heavy-duty industrial machinery, Pargo manages over 10,000 SKUs. Guided by ISO-certified production rigor, continuous R&D investment, and international compliance, Pargo delivers tailored OEM solutions to distributors, brand owners, and industrial clients in over 80 countries.
Custom engineering deployed across critical global sectors and specialized regional climates.
Requirement: Continuous, pulse-free 8.5 bar compressed air for robotic paint spraying and pneumatic torque tools.
OEM Solution: Dual-screw VSD+ systems equipped with integrated desiccant dryers, achieving a PDP (Pressure Dew Point) of -40°C to eliminate micro-blistering in automotive topcoats.
Requirement: Ultra-clean assist gas air supply at 16 to 25 bar pressure, completely free of water and aerosols.
OEM Solution: All-in-one skid-mounted booster compressor packages featuring 5-stage filtration units and high-capacity micro-mist separators.
Requirement: ISO 8573-1 Class 0 oil-free air to satisfy stringent FDA and EMA regulatory compliance.
OEM Solution: Water-lubricated stainless steel scroll compressors utilizing anti-bacterial copper piping and automated sterile purge cycles.
Designed for ambient operating temperatures up to 55°C. Features heavy-duty desert sand pre-filters, oversized aluminum oil coolers, and tropicalized IP65 electrical control boxes.
Engineered for temperatures down to -35°C. Outfitted with automatic crankcase pre-heaters, insulated thermal enclosures, and trace-heated condensate drain valves to prevent freezing locks.
Built with C5-M anti-corrosion marine-grade polyurethane paint coatings, stainless steel fasteners, and salt-mist proof inlet filtration to handle high humidity and offshore salinity.
Pioneering the next decade of intelligent, zero-emission compressed air generation.
The industrial air compressor sector is transitioning from standalone mechanical power units to hyper-connected cyber-physical energy nodes. As factories target Net-Zero carbon emissions, OEM manufacturers must innovate across three critical technological fronts:
Next-generation OEM air compressors come standard with IoT cloud gateway controllers. Utilizing real-time vibration telemetry, oil viscosity degradation sensors, and thermal anomaly detection algorithms, the system predicts bearing wear 500 operational hours before potential failure, eliminating unscheduled factory downtime.
Up to 94% of the electrical energy consumed by an industrial air compressor is converted into heat. Advanced OEM designs integrate thermal energy recovery systems (TERS) that capture waste heat from oil circuits to produce hot water (up to 85°C) for plant heating, boiler pre-heating, or process washing, drastically cutting overall plant energy costs.
Replacing traditional induction motors, future OEM platforms feature Synchronous Reluctance Motors (SynRM). Eliminating rotor copper losses and rare-earth magnet degradation, SynRM technology achieves IE5+ efficiency even at partial load conditions (25% - 50% capacity dynamic range).
Essential criteria for evaluating air compressor manufacturers, supply chain capabilities, and quality assurance protocols.
| Evaluation Pillar | Must-Have Factory Capability | Verification Criteria & Standard |
|---|---|---|
| Machining Precision | In-house CNC rotor grinding & finish turning (FT) | Rotor clearance tolerance within ≤ 0.003 mm; CMM inspection reports provided. |
| Quality System | Full traceably across wire wrapping, welding, and assembly | ISO 9001:2015 certification; 100% full-pressure thermal test bench run before shipment. |
| Compliance Certification | International pressure vessel and safety approvals | ASME Section VIII, CE (PED 2014/68/EU), UL/CSA motor electrical compliance. |
| Supply Chain Depth | Wide SKU breadth and spare parts ecosystem | Availability of matching hardware, tool cabinets, specialized tooling, and fast-ship replacement airends. |
| Customization Agility | Modbus/CANbus smart control & OEM branding options | Custom firmware integration, private label color matching, custom skid dimensioning. |
Expert insights on custom OEM air compressor manufacturing, technical specifications, and ordering protocols.
Explore our broader ecosystem of high-durability mechanical tooling, specialized plumbing sets, and storage systems.





 Pargo Tool